Quality control
Private-label HVAC quality plan: connect the specification to lot release
A final inspection can detect some visible problems in a sample. It cannot repair an incomplete specification, prove every unit conforms or replace control of components, software and production changes.
Sampling supports a defined lot-release decision. It does not establish a universal AQL or prove that every unit conforms.
Turn requirements into measurements
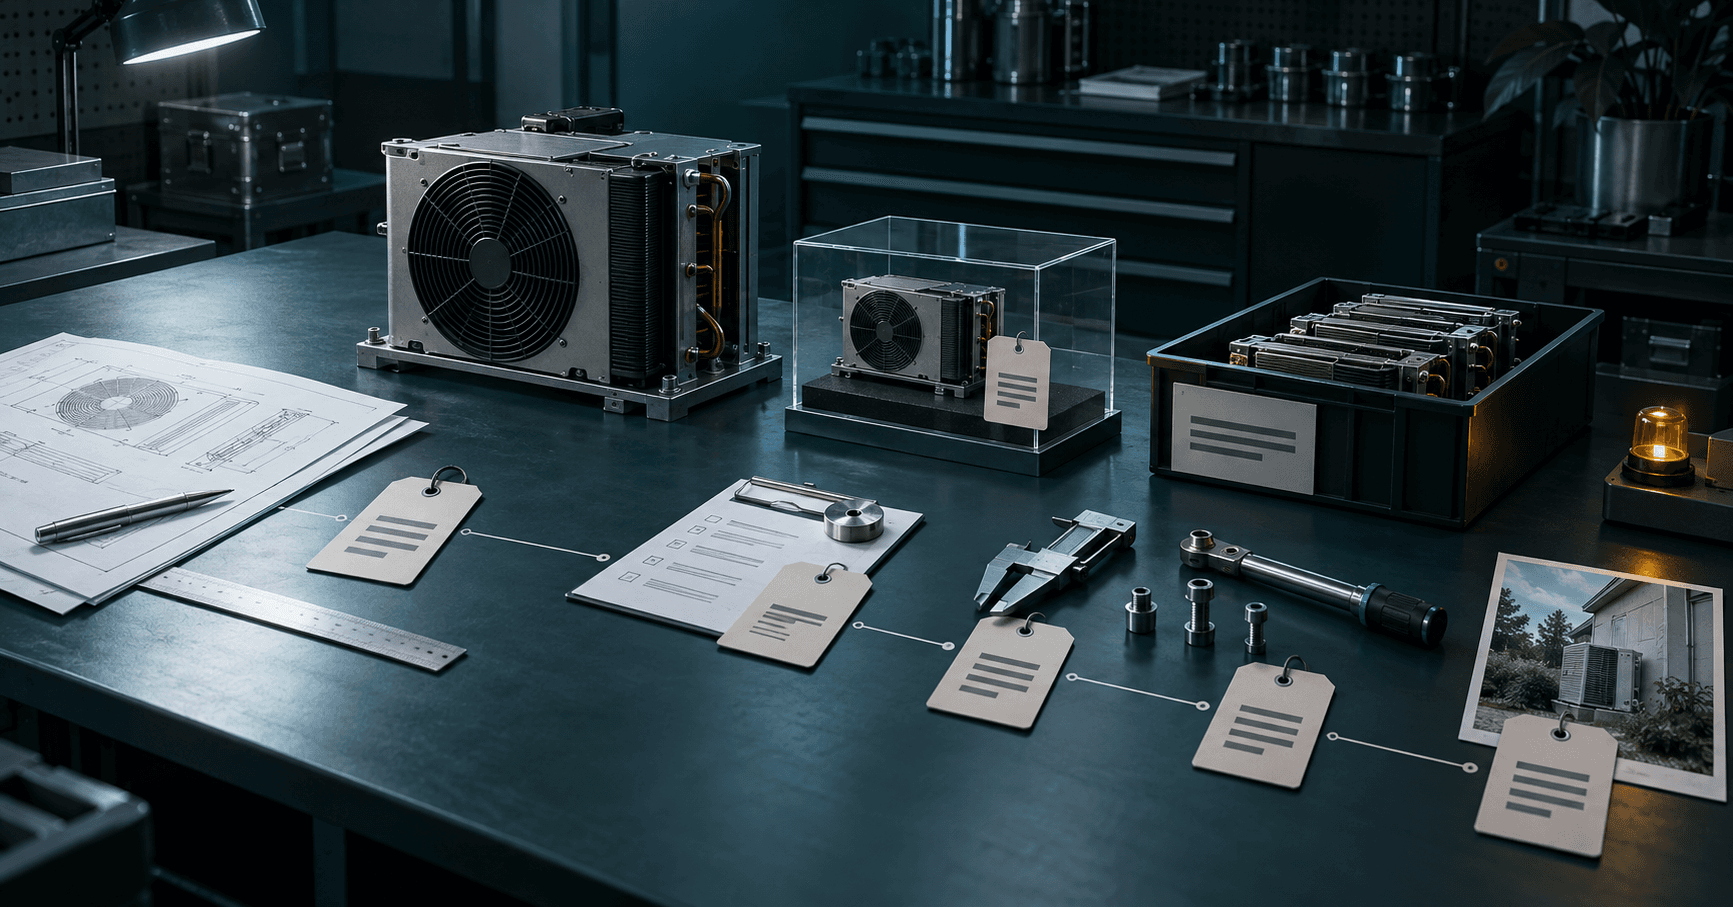
Every critical requirement needs an identifier, revision, measurable target, method, equipment or conditions where material, frequency, acceptance authority and retained record. Separate regulatory and safety requirements from commercial preferences.
‘Quiet operation’ is not an acceptance criterion. A stated measure, condition, configuration and tolerance can become one.
Control the approved reference
Record the golden sample’s model, revision, decisive components, firmware, labels, packaging, accessories and approved deviations. Protect the reference and define who may replace it. A sample does not replace the specification or technical evidence.
Control production changes
- Incoming critical components and assembly processes.
- Refrigerant-system preparation and charging where applicable.
- Electrical, functional, controller and firmware checks.
- Labelling, model identity, packaging and documentation.
- Rework, repair, supplier notification and revalidation triggers.
Define the lot-release decision
Sampling is a decision method, not a quality claim. ISO 2859-1:2026 defines AQL-indexed schemes for lot-by-lot inspection. The parties still need to define the lot, inspection level, defect classification, parameters, switching rules and disposition authority.
Do not copy universal AQL values from a blog. Safety, regulatory, functional, cosmetic and documentation defects have different consequences, and some requirements need different controls or complete testing.
An accepted sample does not prove that every uninspected unit conforms.
Close the field-feedback loop
Connect field failure mode, product identity, batch or serial trace, environment, diagnosis confidence and corrective action. A rare serious or repeated component issue may require faster action than a larger volume of minor presentation defects.
Build the control table
- Requirement and source.
- Product/configuration scope.
- Method, equipment, stage and frequency.
- Acceptance rule and evidence record.
- Reaction, disposition owner and revalidation trigger.
When not to release the lot
- Critical requirements remain descriptive rather than measurable.
- Production cannot be mapped to the approved reference.
- Decisive changes can occur without notification.
- Failed lots can ship through undocumented concessions.
- Traceability cannot connect a field issue to product and batch.
- Product-specific safety or regulatory tests remain unresolved.